 อีเมล: info@guanyumixer.com
หากคุณเคยปรับขนาดสูตรการดูแลส่วนบุคคลจากถังนำร่อง 200 ลิตรเป็นถังผลิตขนาด 5,000 ลิตร เพียงเพื่อจะค้นพบก้อนสารลดแรงตึงผิวที่ยังไม่ละลาย, ฟองอากาศขนาดเล็กที่มีเมฆมาก, หรือความหนืดลดลงกะทันหัน, คุณได้สัมผัสกับความซับซ้อนที่ซ่อนอยู่ในการขยายขนาด. Successful shampoo production line scale-up strategies require precise hydrodynamic control, การถ่ายเทความร้อนที่เหมาะสมที่สุด, and automated raw material handling rather than simply multiplying tank dimensions.
ในตัวเรา 30 years of manufacturing mixing tanks and processing lines for personal care brands worldwide, we have engineered scalable systems for daily chemical plants across 100+ ประเทศ. Formulations containing anionic surfactants, conditioning polymers, and pearlizing agents demand balanced shear profiles to prevent polymer chain degradation while ensuring rapid homogenization.

Why Pilot-Scale Shampoo Formulations Fail During Industrial Production Scale-Up
A common mistake when developing shampoo production line scale-up strategies is assuming that geometric similarity between pilot and commercial vessels preserves flow dynamics. In reality, scaling up tank volume by a factor of twenty while keeping impeller tip speed constant drastically reduces mixing turnover rates and heat exchange surface ratios.
อันดับแรก, surfactant pastes like 70% active Sodium Lauryl Ether Sulfate (สลส) form high-viscosity liquid crystalline gel phases when meeting water. In an oversized tank with basic top agitation, SLES paste clumps into gelatinous fish-eyes that can take hours of wasteful heating and agitation to dissolve.
ที่สอง, high-speed open agitation introduces millions of microscopic air bubbles into the surfactant matrix. Because viscous surfactant solutions hold micro-bubbles in suspension, natural settling can require 24 ถึง 48 hours of holding time, stalling filling line productivity and causing net volume underfills.
Third, salt-adjusted shampoo viscosity is highly sensitive to shear history. Over-shearing through improper transfer pumps or excessive homogenizer cycles breaks polymeric conditioning chains, causing permanent loss of body and product separation in final storage bottles.
Core Shampoo Production Line Scale-Up Strategies for High-Volume Manufacturing
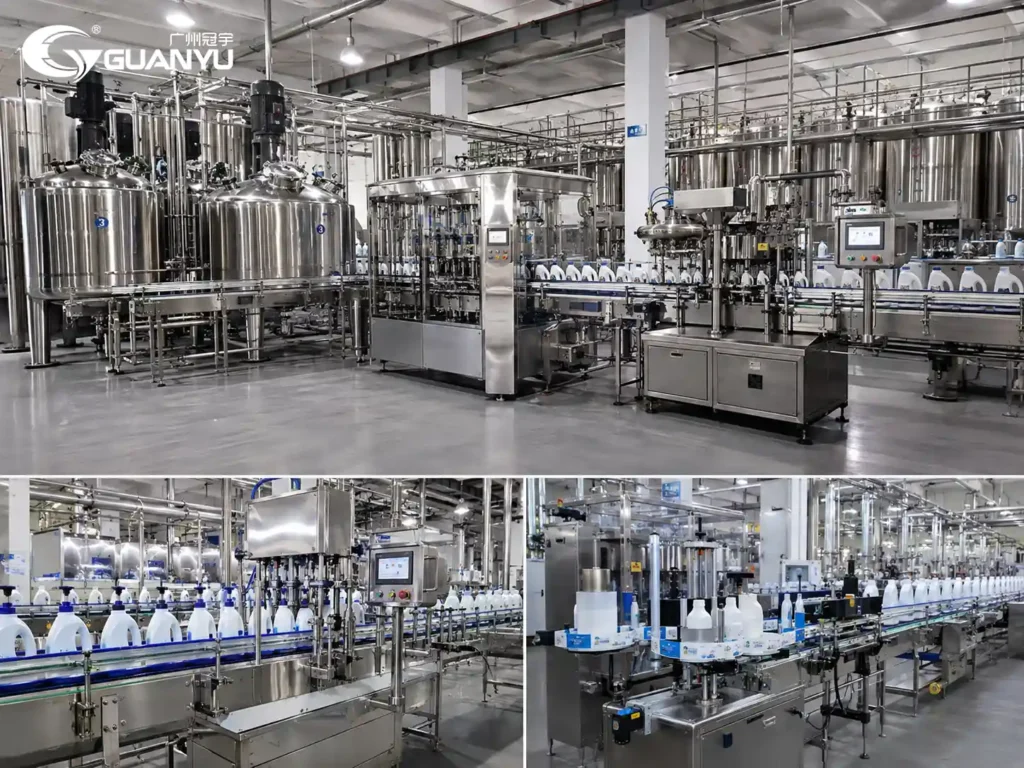
ทันสมัย shampoo production line scale-up strategies integrate modular processing hardware designed around fluid rheology rather than brute mechanical force. Our engineering team designs industrial daily chemical mixing plants with three primary engineering principles.
The first principle is dual-speed counter-rotating agitation paired with dynamic wall scrapers. The outer anchor agitator sweeps the vessel wall with self-adjusting PTFE scrapers to prevent thermal scorching during heating, while inner counter-rotating paddle blades drive downward axial flow into the bottom homogenizer.
The second principle is vacuum-assisted powder and liquid induction. By drawing raw surfactants and thickeners directly beneath the liquid surface under negative pressure (-0.085 MPa), raw ingredients disperse instantly into the turbulent zone without forming floating agglomerates or drawing air into the bulk fluid.
The third principle is variable-frequency drive (วีเอฟดี) control across all mixing stages. In our standard 5,000L mixing vessels, high-shear bottom homogenizers operate at 2,800 RPM during initial phase dispersion and throttle down to gentle recirculation speeds once viscosity-building electrolytes are introduced.
Surfactant Dissolution and Vacuum Deaeration: Solving Aeration and Clumping
In industrial manufacturing trials, การละลาย 70% active SLES into deionized water represents the largest energy and time bottleneck. In our 5,000L shampoo batch dissolution trials, vacuum powder induction at -0.085 MPa completely wetted 70% active SLES paste in under 18 minutes without fish-eye formation.
Operating under continuous vacuum also eliminates entrained air at the source. As volatile fragrances and pearlizing concentrates blend at 45°C, vacuum deaeration strips micro-bubbles instantly, allowing the finished shampoo to transfer directly to packaging buffers without overnight holding.
For facilities expanding into adjacent categories, this processing architecture aligns directly with liquid soap production line automation และ สายการผลิตครีมและโลชั่นอัตโนมัติ ระบบ. It allows plant managers to standardize operational procedures, spare parts inventories, and operator training across multiple production halls.
Batch vs Continuous Mixing: Technical and Economic Comparison Table
Choosing between multi-vessel batch mixing and continuous inline blending depends on SKU diversity, batch volumes, and changeover frequency. The comparison table below highlights key performance metrics for commercial scale-up planning.
| Operational Factor | Single Multi-Function Mixing Tank | Multi-Vessel Batch Plant (Pre-mix + Main) | Automated Continuous Inline Mixing Line |
|---|---|---|---|
| Batch Capacity Range | 500ล – 3,000L per batch | 3,000ล – 10,000L per batch | 5,000 – 25,000 L/hour continuous |
| Batch Cycle Time | 2.5 – 3.5 ชั่วโมง | 1.2 – 1.8 ชั่วโมง (staggered) | Continuous non-stop flow |
| Surfactant Wetting Method | Top charge + homogenizer ด้านล่าง | Vacuum induction manifold | High-shear inline dynamic mixer |
| SKU Flexibility / Changeover | สูง (30 min clean between colors) | ปานกลาง (45 min CIP routine) | ต่ำ (requires dedicated high-volume runs) |
| Deaeration Mechanism | Vessel vacuum deaeration | Full vacuum processing tank | Inline continuous vacuum deaerator |
| การลงทุนด้านทุน & ROI | Lowest initial entry cost | Optimal for 10-30 tons/day | High output for national brands |
Integrating centralized SCADA recipe management with ระบบควบคุมอัจฉริยะสำหรับไลน์อิมัลชัน allows operators to recall validated mixing times, อุณหภูมิ, and shear speeds at the push of a touchscreen button. This automated parameter recall prevents human batch setup errors and ensures identical surfactant hydration across every production shift.

Automated CIP/SIP and Temperature Control for Rapid Batch Changeovers
Contract packagers and brand owners frequently run multiple shampoo variants—such as clarifying formulas, sulfate-free blends, and anti-dandruff treatments—through the same mixing hardware. Maintaining high plant overall equipment effectiveness (อีอี) requires rapid, automated cleaning changeovers.
Our mixing tanks feature rotary 360-degree spray balls delivering wash solution at 0.35 MPa across all internal vessel surfaces. In our factory cleaning validation protocols, automated alkaline wash and hot water rinse cycles reduced changeover downtime from 110 minutes of manual scrubbing to just 28 minutes of hands-free CIP.
Thermal management relies on dimple jacket cooling with turbulent glycol or chilled water channels that cool 5,000-liter batches from 75°C to 30°C in under 35 นาที. As recommended in the ISO 22716 Cosmetics Good Manufacturing Practices, validated automated cleaning routines ensure microbiological compliance and prevent color or fragrance carryover.
Supplier Audit Checklist: 5 Documents to Request Before Scaling Your Shampoo Line
Before approving equipment procurement or releasing capital milestone payments for your personal care mixing line, require the following technical verification files from your machinery builder. Rigorous engineering documentation ensures that your mixing vessels comply with international pressure vessel and sanitary codes:
- 1. Material Test Certificate (MTC 3.1) verifying SUS304 jacket and SUS316L product contact construction with Ra ≤ 0.4 μm mechanical polish or Ra ≤ 0.28 μm electropolish.
- 2. Hydrodynamic Impeller and Homogenizer Power Curve Calculations verifying motor torque and shear rate suitability across your product’s full viscosity spectrum (1,500 cP to 18,000 ซีพี).
- 3. Vacuum Integrity and Vessel Pressure Certificate proving vessel containment under -0.09 MPa vacuum and +0.2 MPa jacket working pressure according to ASME or PED codes.
- 4. Automated CIP Riboflavin Spray Coverage Test Protocol demonstrating 100% internal surface coverage and complete drainability through bottom diaphragm valves.
- 5. บมจ & SCADA Functional Specification and Batch Recipe Code Documentation with multi-level operator access control and batch data logging.
คำถามที่พบบ่อย: Key Questions on Shampoo Production Line Scale-Up Strategies
How can we prevent viscosity variation between different 5,000L shampoo batches?
Viscosity inconsistency is typically caused by uncalibrated manual salt dosing, uneven batch cooling, or variable raw surfactant active concentrations. In our automated mixing systems, we integrate inline Coriolis mass flow meters and loss-in-weight electrolyte dosing feeds linked directly to PLC recipe controls. When auditing suppliers, require automated gravimetric raw material metering rather than manual bucket additions.
What is the best way to incorporate heat-sensitive active botanical extracts and fragrances?
Active botanicals and volatile fragrance oils must be introduced after the main batch has cooled below 40°C to prevent thermal degradation and flash evaporation. Our vessels utilize a dedicated secondary additive port with bottom vacuum suction to draw delicate actives into the bulk liquid while gentle paddle agitation ensures uniform distribution without high shear. Always verify that your mixing system features automated cooling temperature interlocks before fragrance addition.
Is high-shear homogenization always necessary for clear shampoo formulations?
High-shear homogenization is essential during the initial surfactant wetting and polymer hydration phases to disperse clumps without heating delays, but must be throttled down or bypassed once electrolytes are added. Our GY series mixers feature frequency-inverter homogenizers that can switch between high-intensity bottom shear and gentle low-shear loop circulation depending on the recipe stage. Ensure your machinery vendor provides multi-speed recipe programming.
How much floor space and ceiling height are required for a 5,000L shampoo mixing plant?
A standard 5,000L commercial mixing vessel with integrated maintenance platform, raw material pre-mix tanks, and vacuum transfer pumps requires approximately 35 square meters of cleanroom floor space and a minimum ceiling clearance of 4.8 เมตร. In our engineering practice, we provide complete 3D factory layout drawings and piping isometric designs to optimize operator ergonomics and material flow. Request full 3D CAD modeling from your supplier before finalizing civil works.